Reliable Precision Subcontractor for Tool Shops
Precision Machining Articles
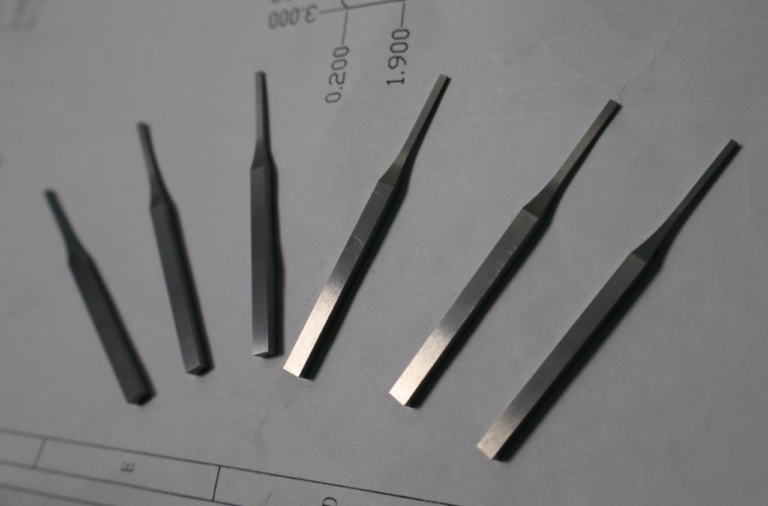
How to Reduce Distortion in Thin Stamping Punches
Thin precision tooling components can be difficult to keep dimensionally stable during machining. Even when the required dimensions are achievable, a part may bend, twist or change shape during material removal or…
Precision Punch Manufacturing: From Preparation to Profile Grinding
Precision punch manufacturing involves more than machining a part to its nominal dimensions. For stamping die applications, the manufacturing route must account for material properties, geometry, critical tolerances and the functional requirements…

Punch Profile Design: Sinker EDM or Profile Grinding?
A small change in punch geometry can sometimes lead to a significantly different manufacturing process. Recently, we received a stamping die punch drawing with a stepped transition in an approximately 11 mm…
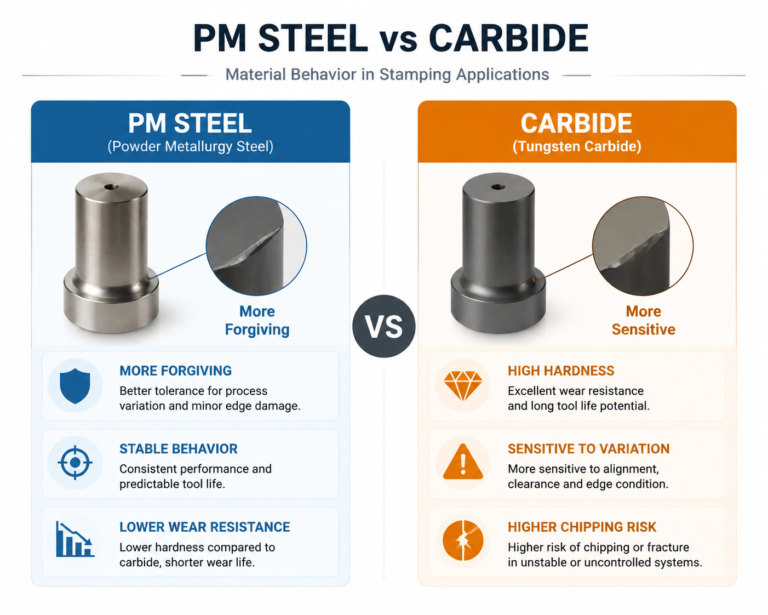
Carbide Punches for Copper Alloy Stamping: Why System Stability Matters More Than Material Alone
In many stamping applications, upgrading from PM steel to carbide is considered a straightforward improvement. Higher hardness. Higher wear resistance. Longer tool life. From a material perspective, the logic seems obvious. However,…
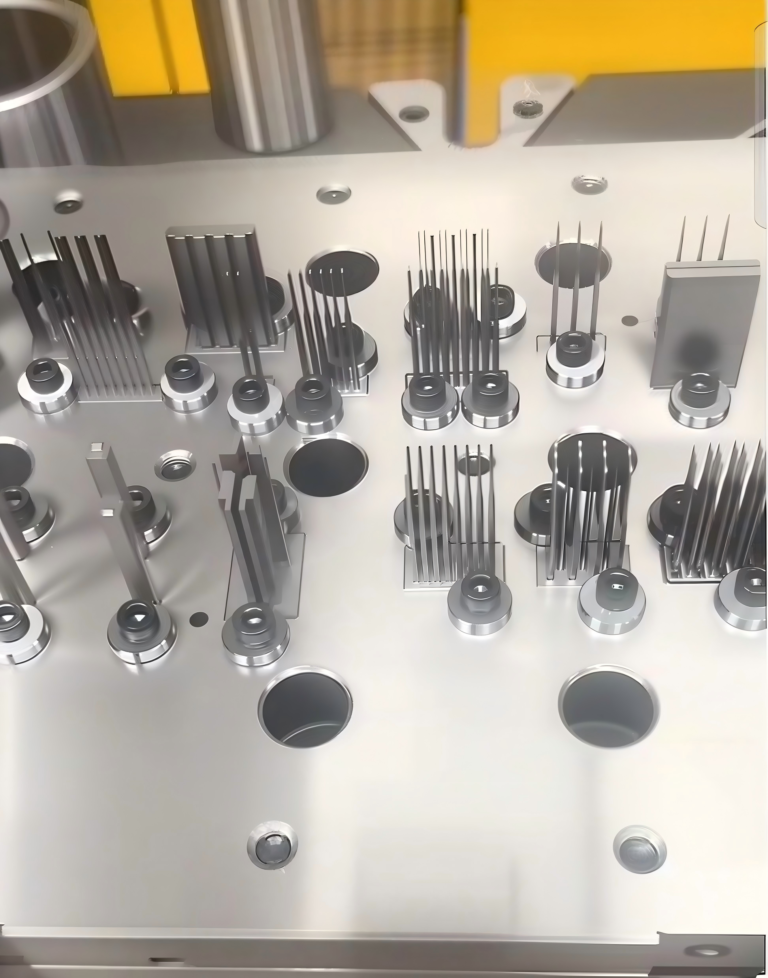
Why Connector Tooling Has Become More Demanding Even When Drawings Haven’t Changed
Over the years, one thing has become increasingly noticeable in connector tooling work: The drawings often look almost the same as they did years ago. The dimensions, the basic geometry, even the…
Carbide Grade Selection for Stamping Dies: Follow the Print or Evaluate Alternatives?
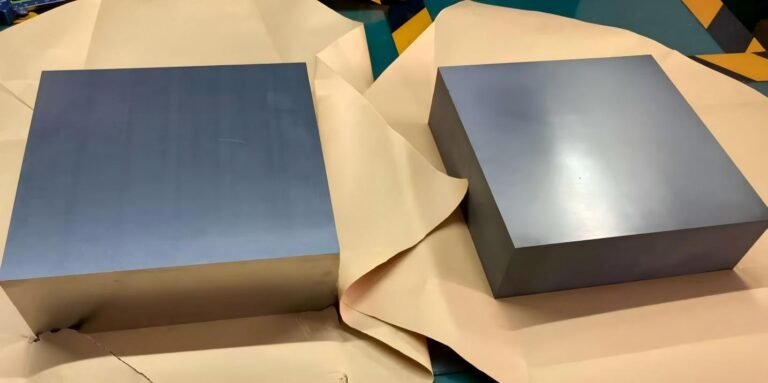
Selecting the right carbide grade is one of the most important decisions in precision stamping tooling. The wrong grade can lead to premature wear, edge chipping, unexpected downtime, and increased maintenance costs.…
The Fragile Reality of ±0.002mm Batch Consistency in Micro Punch Grinding
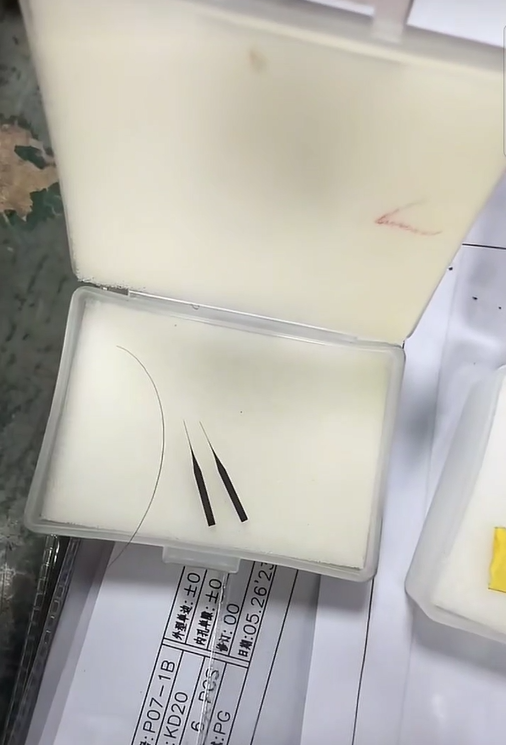
A sudden cough, an extra gust of AC air, or a tiny temperature fluctuation—in the world of micro punch grinding, that is all it takes to turn an expensive piece of Tungsten…
Case Study: The Hidden Reason Behind Metal Slivers and Die Dust in High-Speed Stamping
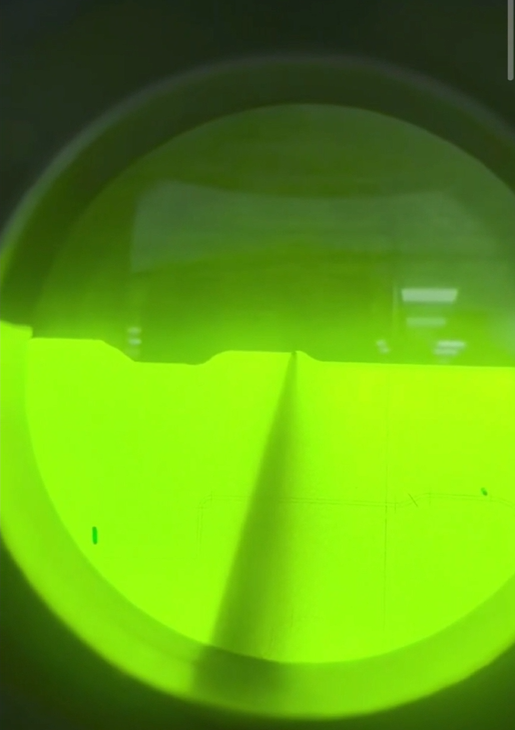
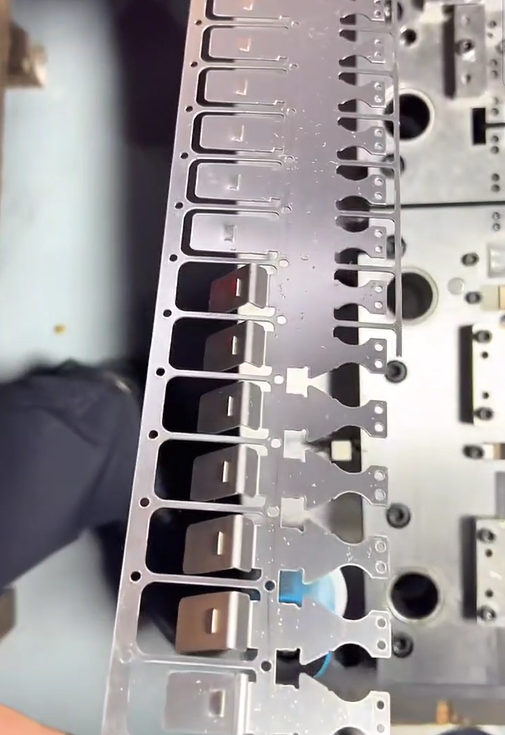
We brought their current punches into our testing lab and inspected the flanks under a 50x projector. The inspection revealed that the root cause wasn’t the press parameters, material hardness, or lubrication…
Why Precision PG Grinding is the Only Way to Offset Rising Carbide Costs
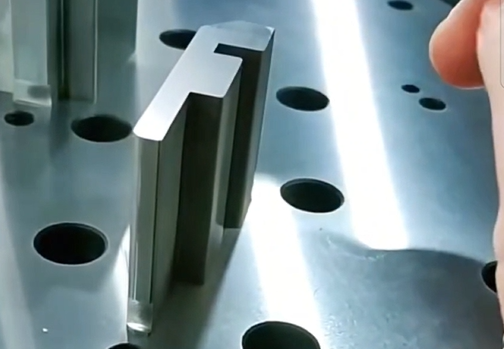
In the current manufacturing landscape, Tungsten Carbide is no longer just a raw material—it is a significant capital investment. With prices steadily climbing, treat every carbide punch and insert as a high-value…
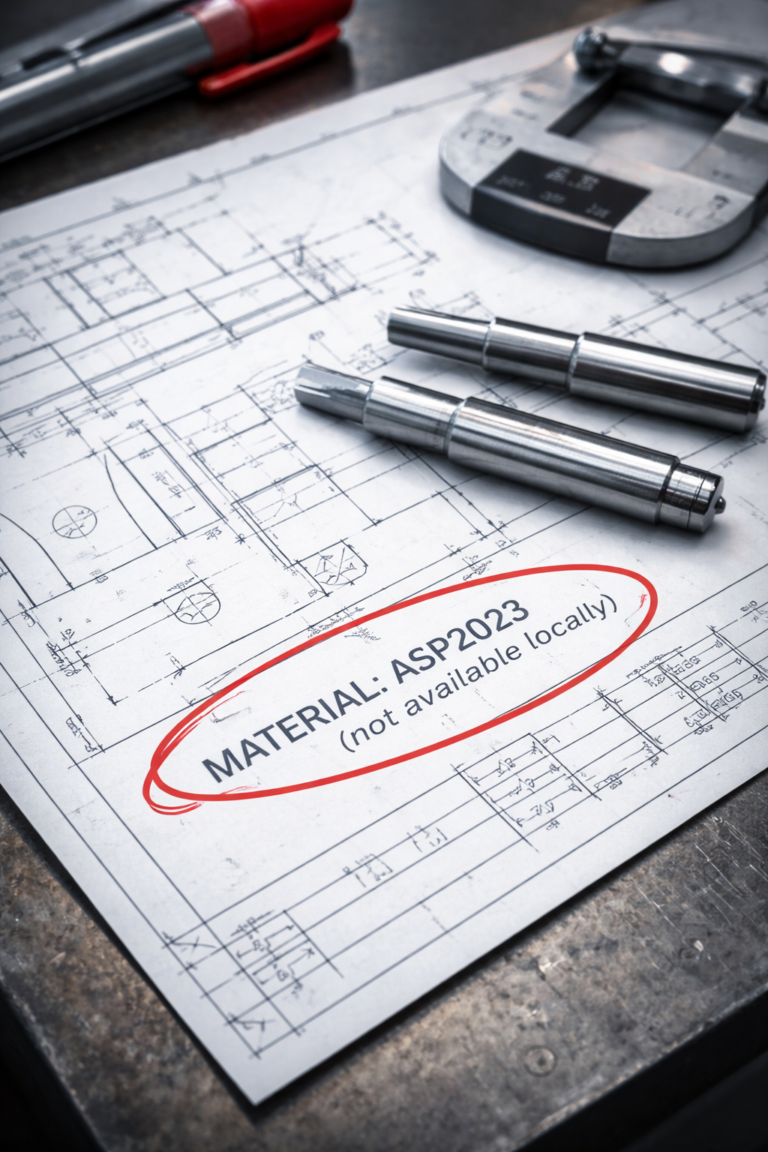
What If Tooling Material Is Not Available?
Material availability issues are quite common in tooling projects. Drawings may specify certain grades that are difficult to source locally, have long lead times, or are no longer widely used. This is…
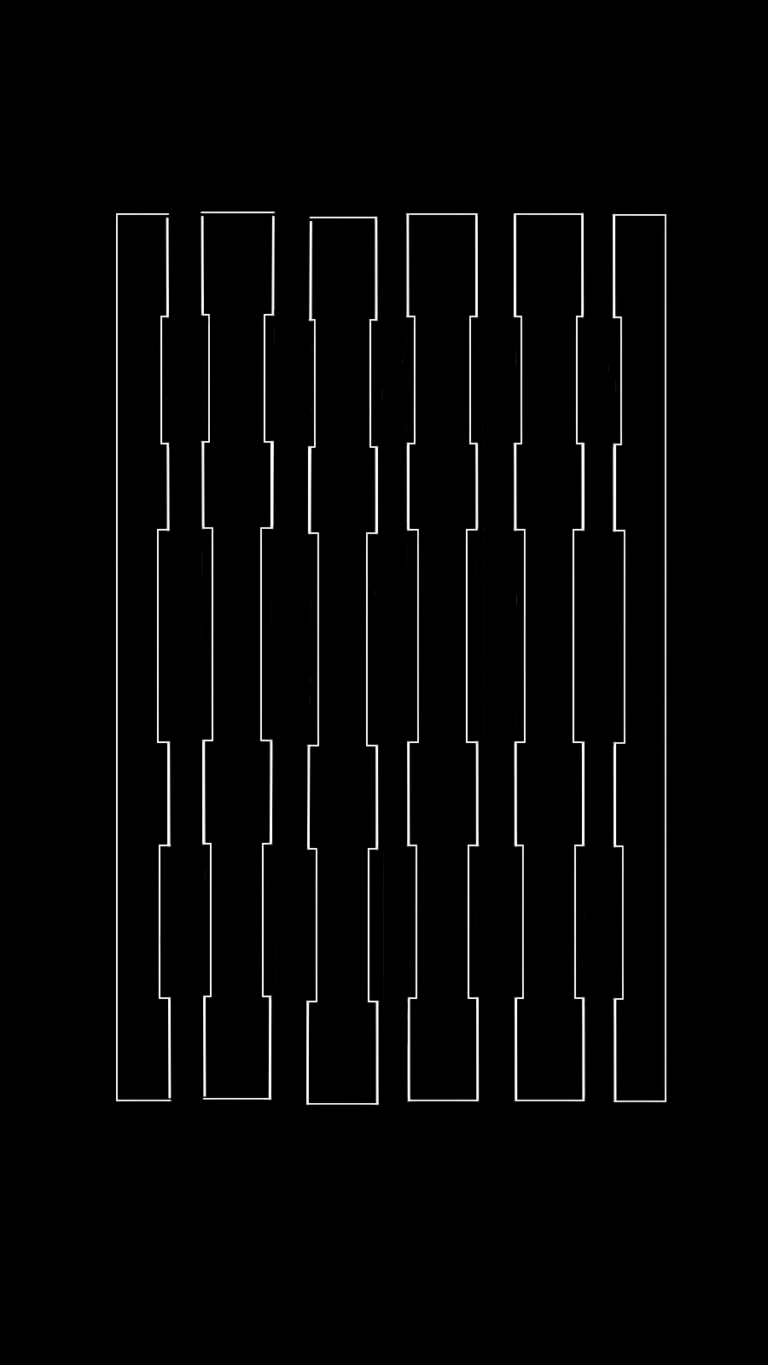
Segmented Tooling Design vs Wire EDM: How PG Grinding Reduces Cost
This results in: Segmented tooling design offers a different approach. Instead of manufacturing a component as a single unit, the structure is divided into multiple functional segments. Each segment can be individually…
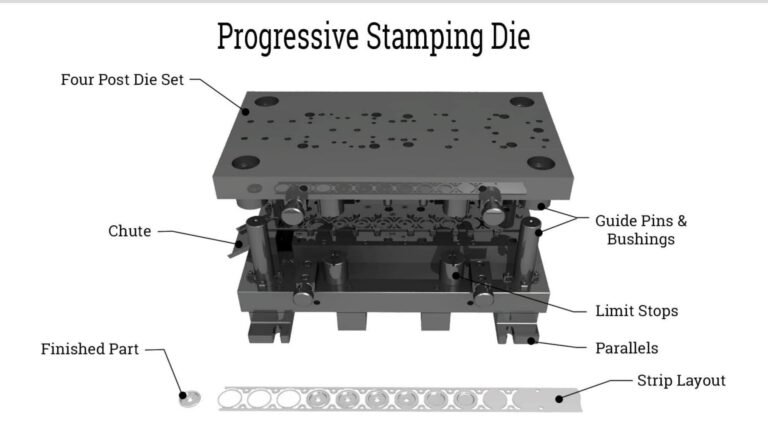
When Shear Angle Looks Right but Stamping Stability Still Fails
In many progressive die applications, shear angle is often treated as a secondary detail — mainly used to reduce cutting force or extend tool life. But in real production, its impact goes…
 English
 Korean
 Japanese
 Spanish
 Portuguese
 French
 German